Qingdao Better International Corporation supplies organic peroxide initiators, ion exchange resins and specialty water-treatment chemicals to polymer, rubber, water-treatment and industrial customers worldwide.
Qingdao Better International Corporation (青岛铂特进出口贸易有限公司) is a China-based supplier of specialty chemicals, serving customers in the polymer, rubber, coatings, composites, water-treatment, power-generation and pharmaceutical industries.
We focus on three principal product families: organic peroxide initiators and crosslinking agents, ion exchange resins, and specialty water-treatment chemicals and protective materials. Our products support applications ranging from LDPE and PVC polymerization, unsaturated polyester curing and rubber vulcanization, through to ultrapure water production, wastewater purification, hydrometallurgy and marine antifouling.
Reliable supply is the foundation of our business. We work closely with established manufacturing partners and accredited testing laboratories in China, integrating their production capacity, technical expertise and quality systems into a single, dependable service for our international customers.
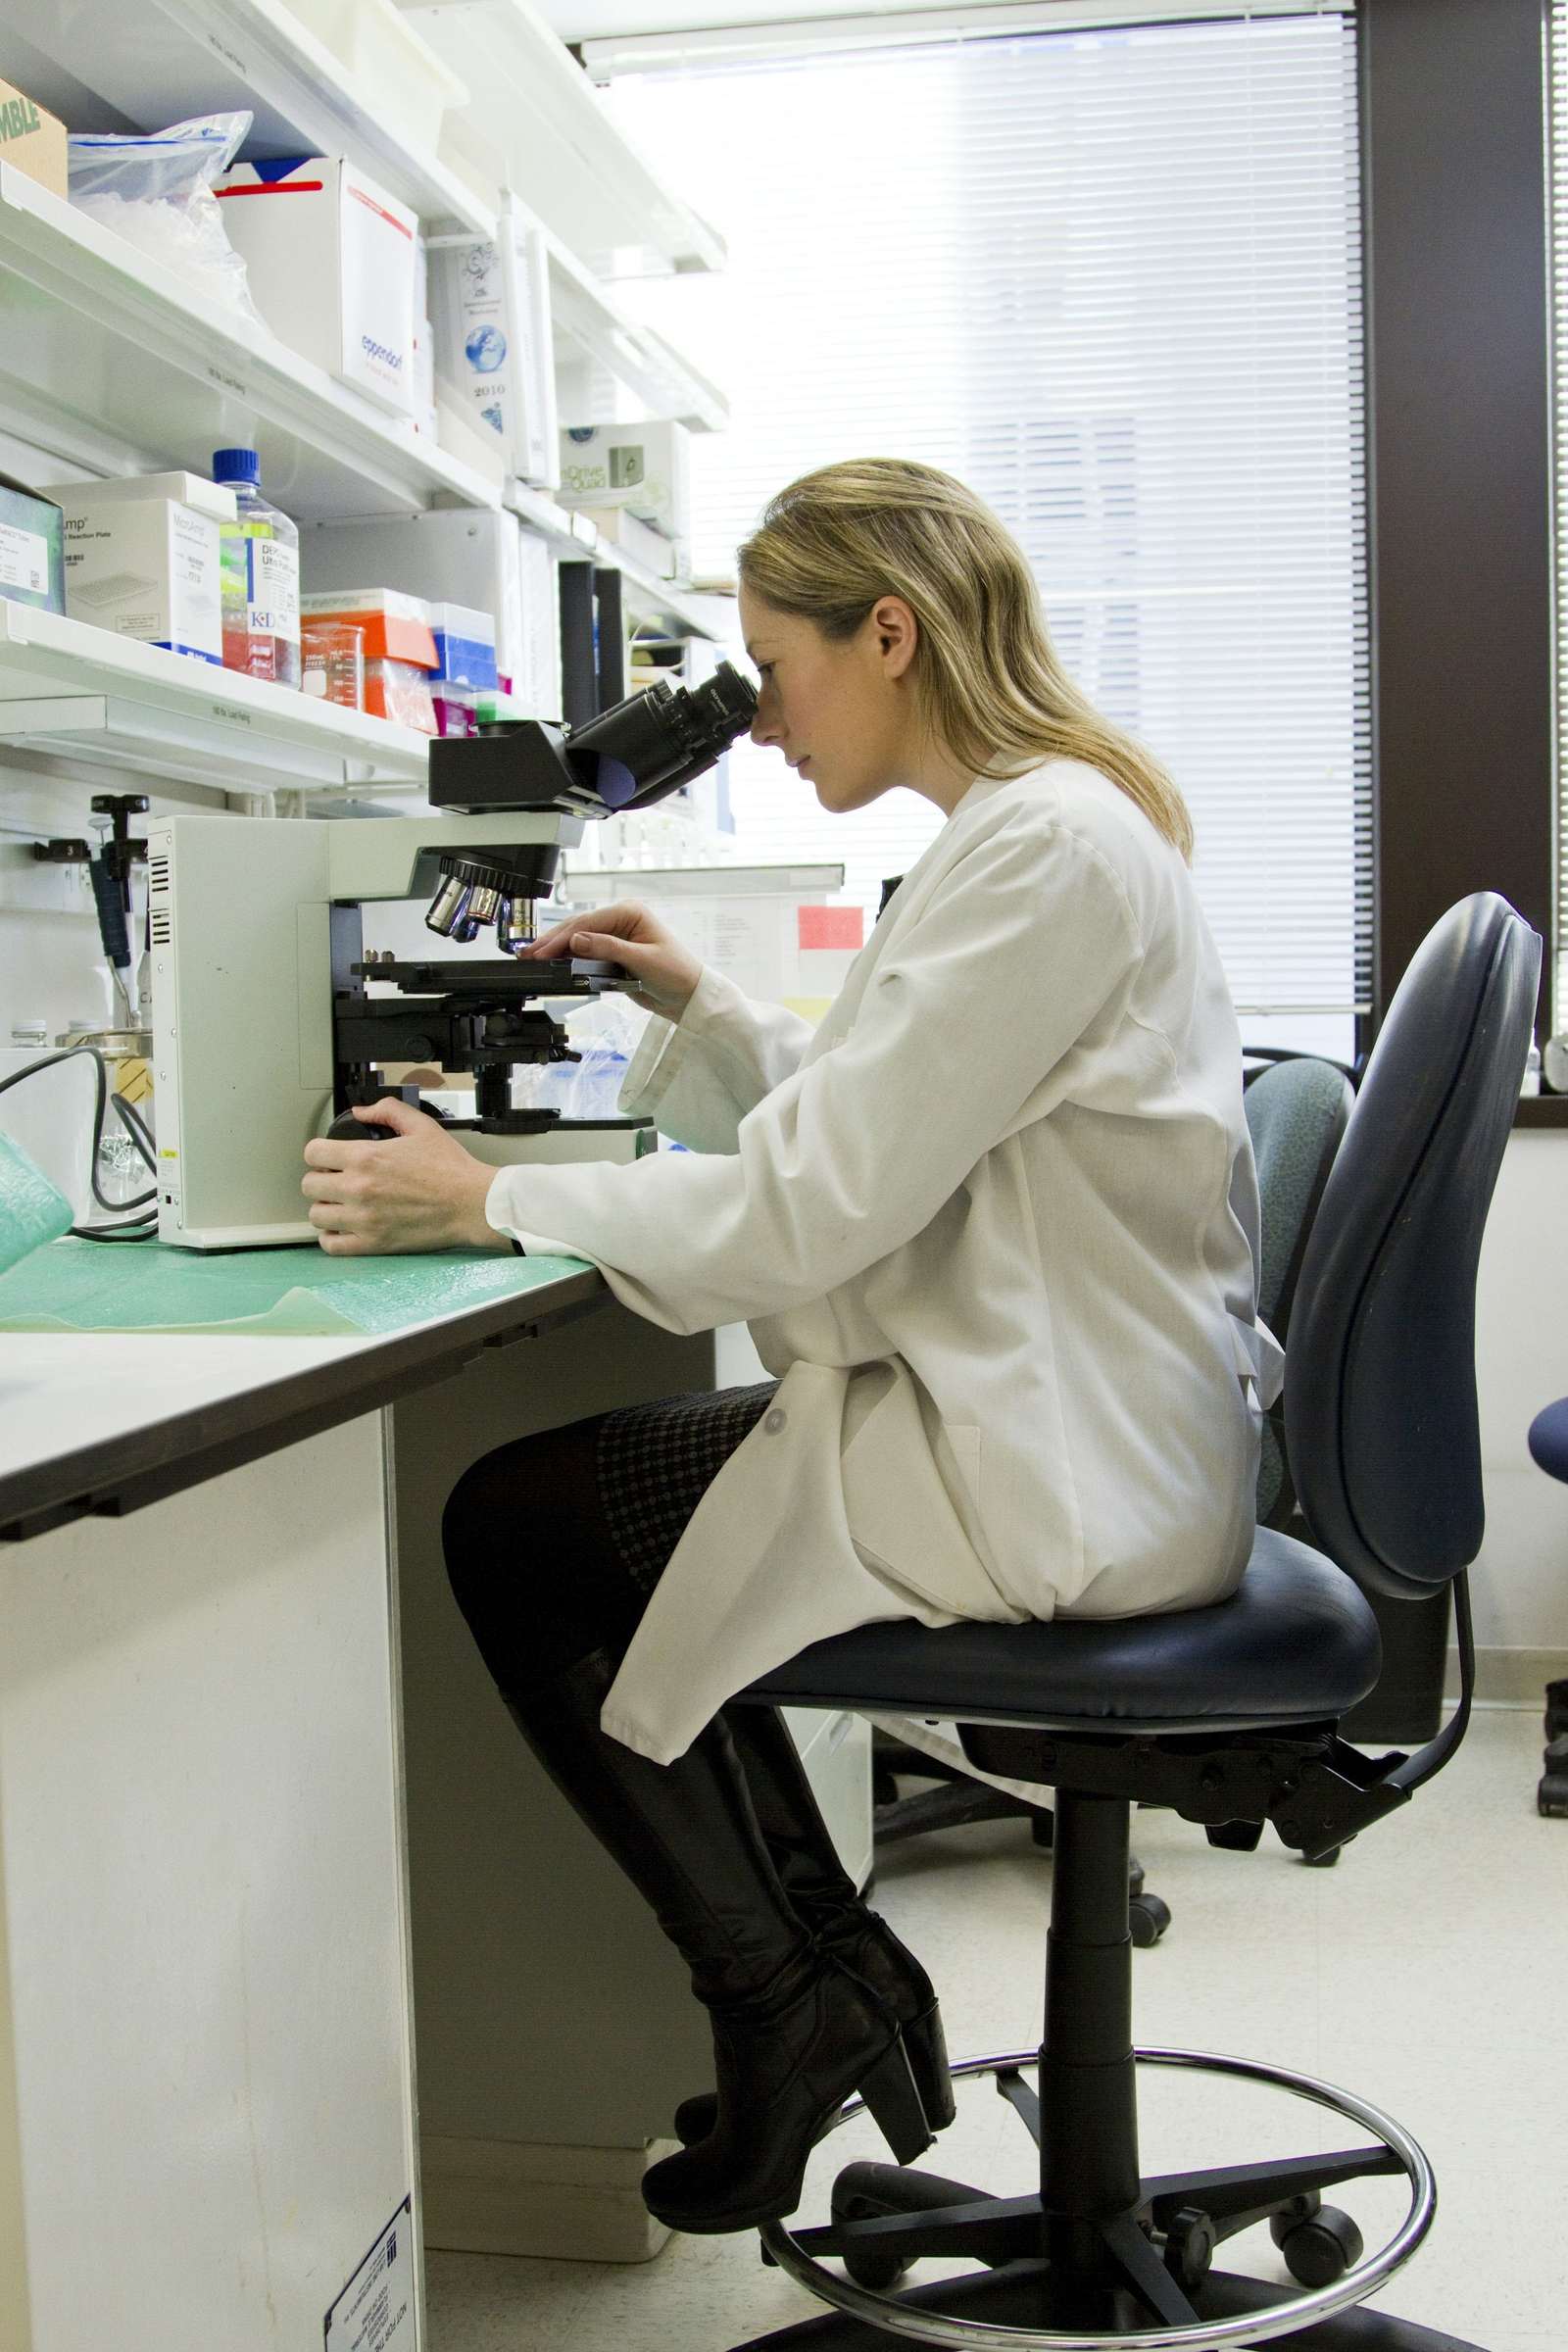
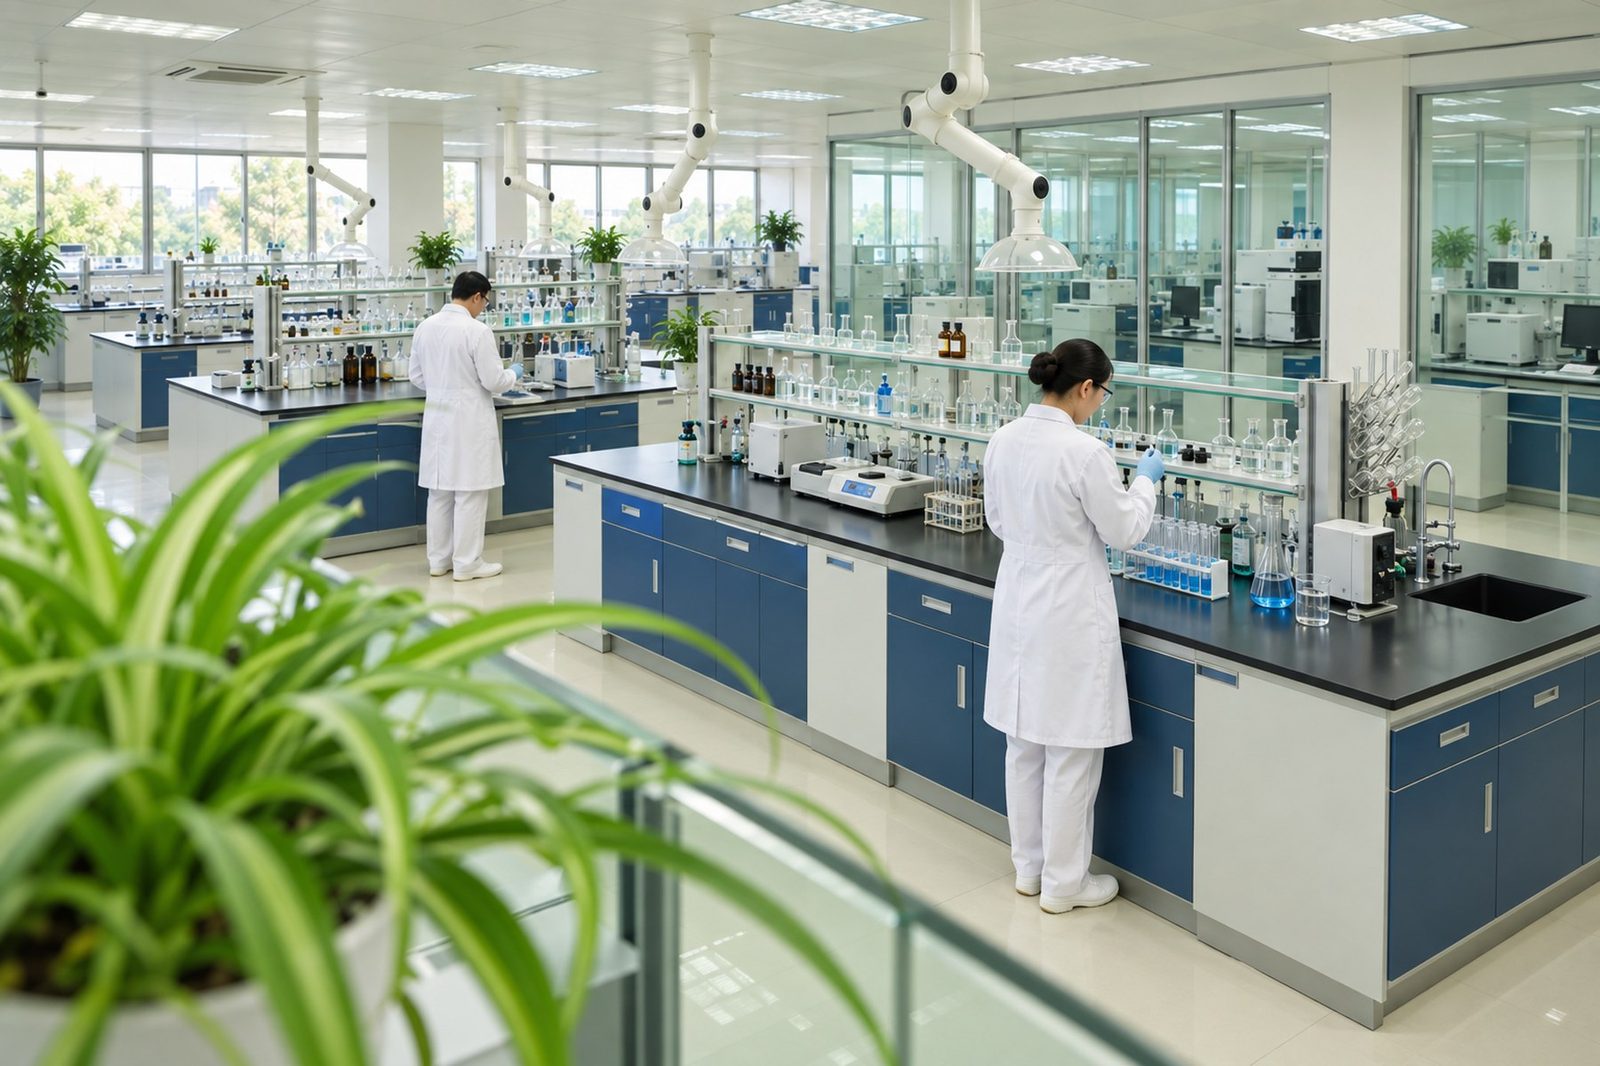
Our partner facilities include a dedicated water-chemistry laboratory and calibration & testing centre, established within China's shipbuilding research system. It is the specialised entity devoted to water-quality treatment and detection, and has held CNAS accreditation since 2020, authorised for 14 testing items including ion exchange resin performance testing.
Approximately 900 m² of supporting test infrastructure is equipped with dedicated benches for resin preparation and regeneration treatment, water-production technology (RO + EDI), condensate-water purification, and power-system cleaning and descaling.
Analytical capability covers resin characterisation, water-quality supervision and materials analysis — including ion chromatography, gas chromatography, organic carbon analysis, UV/Vis and atomic absorption spectrophotometry, and ultrapure water production.
Self-developed resin products are benchmarked directly against imported equivalents, and are fully up to or better than imported products across key indicators — including uniformity coefficient, sphericity, exchange capacity, conversion rate and high-temperature attrition loss.

A dedicated calibration and testing centre of approximately 900 m², equipped with benches for resin preparation and regeneration treatment, RO + EDI water-production technology, condensate-water purification, and power-system cleaning and descaling.
Comprehensive analytical capability supporting resin characterisation, water-quality supervision and materials analysis:
Continuous development across the full specialty-chemicals spectrum:
Self-developed resin products are benchmarked directly against imported equivalents, and are fully up to or better than imported products across key indicators — including uniformity coefficient, sphericity, exchange capacity, conversion rate and high-temperature attrition loss.
Our organic peroxide supply is supported by a production facility that researches, develops, manufactures and sells organic peroxide initiators, curing agents, catalysts and vulcanizing agents.
An annual organic peroxide production capacity of approximately 10,000 tonnes, with capability across 30 types of organic peroxide products and the ability to supply and export additional Class 5.2 products. Factory cover area of approximately 2,000 m², with cumulative investment in the region of RMB 20 million.
Production facilities are designed by leading chemical design institutes to international first-class standards for safety and process flow. The plant adopts a DCS automation control system for centralised control, complemented by an SIS safety instrumented system for centralised detection, display, interlock and control of major-hazard installations.
A sound product-quality assurance system, advanced production technology and complete analytical and experimental instruments. All production facilities are ISO 9001 certified, ensuring the highest product quality and strict compliance with environmental regulations.
A mature, reliable and advanced process technology operating safely for many years, with high product quality and low production pollution. A high level of automation and machinery with well-sealed equipment underpins stable, consistent output for export markets worldwide.
Our portfolio covers three core product families. Representative product groups are listed below — the complete range of 111 products is available in our product catalogue.
Our products are used across a broad range of industries and process technologies.